ABEL Pumps
High-Pressure Piston Diaphragm & Solids Handling Positive Displacement Pumps
ABEL Pumps
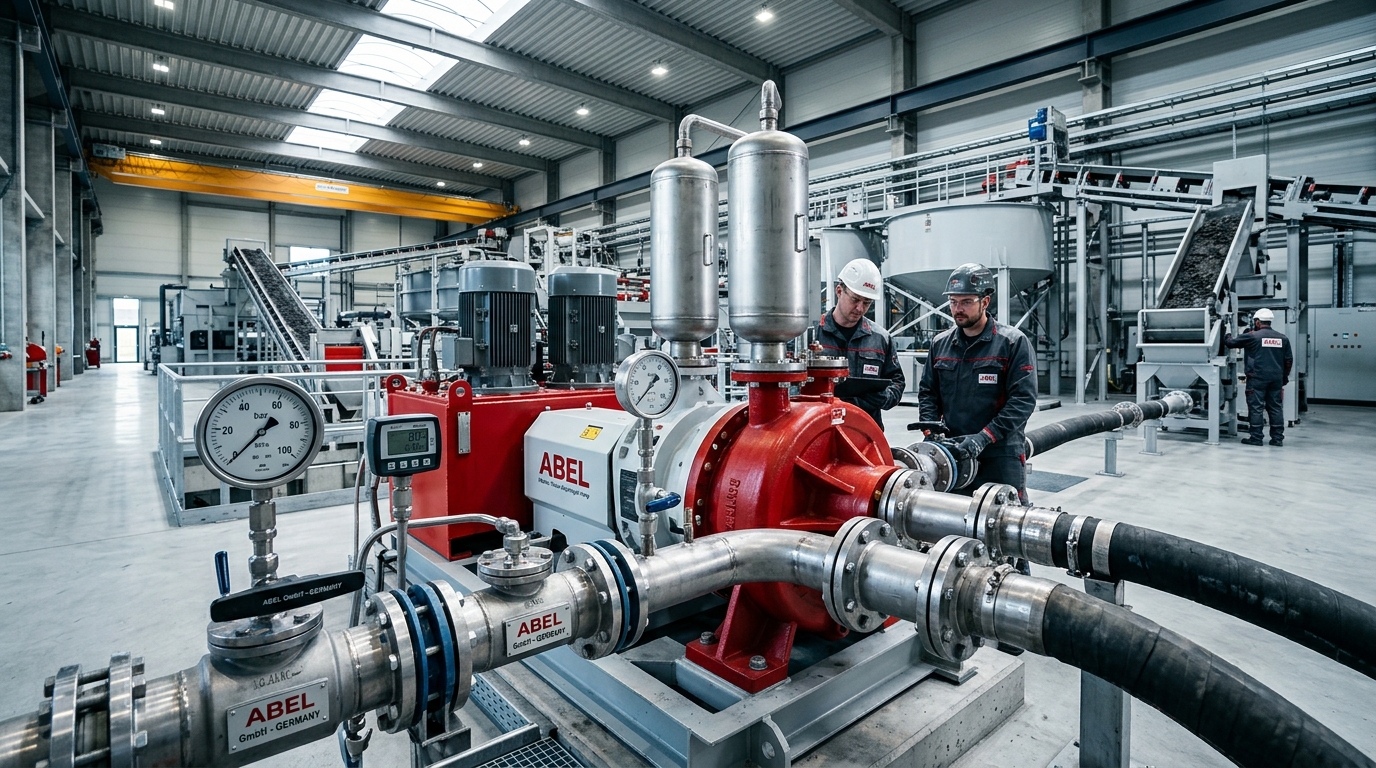
ABEL GmbH is a worldwide leader in high-pressure reciprocating positive displacement pumps. Specialized in severe abrasive slurries, high solid content media up to 80%, and filter press feeding, ABEL pumps deliver unrivaled mechanical longevity and mechanical efficiency exceeding 90%.
Model Lookup Matrix for ABEL High-Pressure Pumps
Hermetic Hydraulic Diaphragms
Pistons actuate solely on clean hydraulic fluid, isolating aggressive slurries completely from mechanical cylinders and multiplying service intervals.
Smart Filter Press Feed Control
Integrated pressure-sensing regulation automatically shifts from high flow to high pressure as cakes densify, maximizing dryness and cycle times.
Wear-Resistant Valve Technology
Heavy-duty polyurethane and solid ceramic ball/cone valves ensure tight positive shut-off even in media loaded with coarse gravel and fibers.
Core Product Series & Technical Specifications
ABEL EM Series Electromechanical Pumps
Energy-efficient mechanical diaphragm pumps for high-viscosity sludge, lime milk dosing, chemical feed, and wastewater transfer up to 16 bar.
ABEL HM & CM Hydraulic Diaphragm Series
Heavy-duty single and double-acting piston diaphragm pumps engineered for abrasive mineral slurry transfer, spray dryer feeding, and filter press feed up to 100 bar.
ABEL SH & HP High-Pressure Solids Series
Cone-valve hydraulic piston pumps moving paste-like dewatered sewage cake, mineral backfill, and dense solid media up to 80% solid concentration.
Explore Other Strategic OEM Partners
SonFlow A/S
High-Efficiency Plate Heat Exchangers & Free-Flow Thermal Systems
DanPumps A/S
Heavy-Duty Centrifugal & Submersible Wastewater Pumping Solutions
Alfa Laval
Global Leader in Heat Transfer, Separation & Sanitary Fluid Handling
Mehrer Compression
100% Oil-Free Reciprocating & Diaphragm Process Gas Compressors