Food Side-Stream Valorisation: A Resilient Food System

Transforming industrial food processing side streams (brewery spent grains, citrus and fruit pomace, coffee grounds, acid whey) from waste disposal liabilities into high-value commercial ingredients (pectin, antioxidants, concentrated proteins, and renewable biogas) represents the vanguard of the circular bio-economy. Lecoqimex delivers an integrated engineering portfolio: non-clog SonFlow Free Flow wide-gap plate heat exchangers for coarse fibrous suspensions, heavy-duty ABEL HM piston diaphragm pumps feeding thick pastes into filter presses, and Mehrer 100% oil-free compressors capturing bio-methane gas securely.

Food Side-Stream Valorisation: A Resilient Food System

Monetizing Organic Side Streams & Slashing Industrial Sludge Disposal Costs

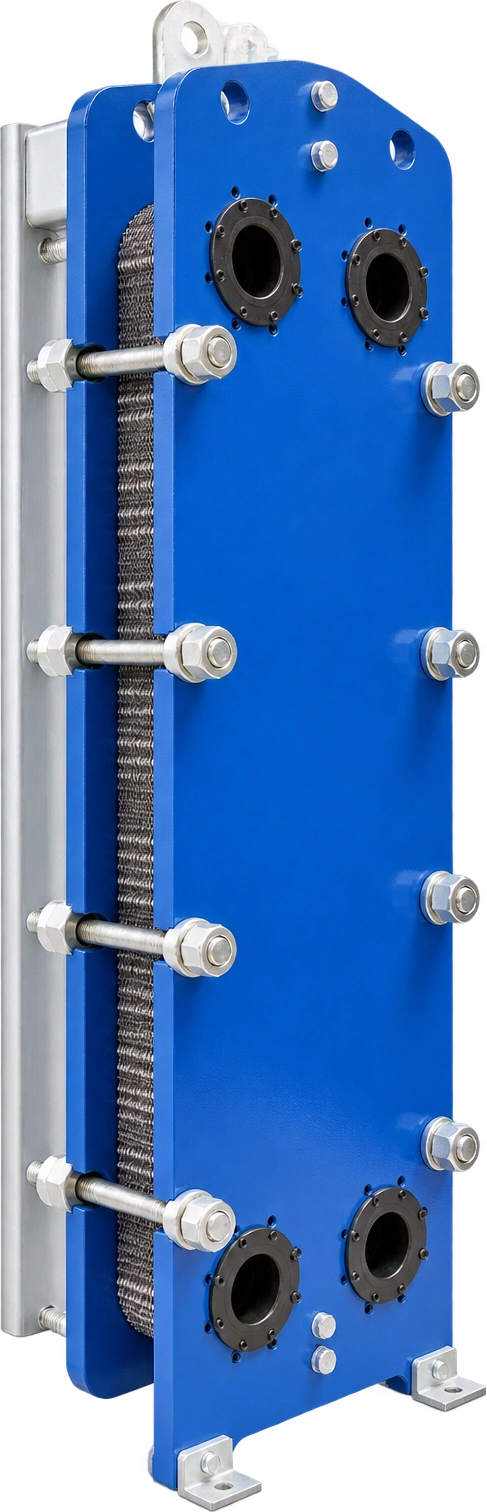
  • SonFlow Free Flow plate heat exchangers extracting polyphenols and pectins without channel clogging
  • ABEL HM piston diaphragm pumps moving heavy slurries and pastes with dry solids content up to 35-40% DS
  • Mehrer 100% oil-free compressors boosting raw biogas pressures for boiler firing and CHP engines
  • Hermetic continuous thermal loops preserving raw side streams against rapid microbiological spoiling

In many conventional food and beverage facilities, valuable side streams such as spent grains or citrus peel are mixed haphazardly into a common effluent sump, destroying valuable ingredient potential while triggering rapid foul fermentation. By segregating clean side streams directly at machine outlets and passing them through SonFlow Free Flow plate exchangers for thermal stabilization or extraction, processors capture valuable bio-actives. Dewatered fiber cakes from ABEL pumps serve as biomass fuel or feed anaerobic digesters for green energy.

1. Principles of Side-Stream Segregation & Biological Integrity

In the era of Industrial Transformation and ESG stewardship, the concept of "food waste" is being actively redefined into "secondary high-value bio-feedstocks".

Processing side streams from breweries (spent grains rich in protein and beta-glucan fibers), juice mills (citrus peel and apple pomace packed with pectin and polyphenolic antioxidants), sugar mills (bagasse), and dairy dairies (liquid whey) represent lucrative ingredient streams if segregated cleanly at the machine boundary and thermally conditioned against microbial decay. Lecoqimex provides synchronized European process systems uniting SonFlow, ABEL, and Mehrer to unlock this circular potential.
1. Principles of Side-Stream Segregation & Biological Integrity
Fig 1.1: Conceptual material pathway from clean side-stream segregation to value-added nutrient recovery.

2. The Integrated Side-Stream Valorisation Process Sequence

Standard industrial food side-stream valorisation is deployed across five synchronized stages:

Stage 01

Segregated Collection & Thermal Stabilization

  • 01. Closed Machine Interception: Diverting streams directly from decanters/filters before contact with plant drainage.
  • 02. Rapid In-Line Chilling: SonFlow PHEs chill wet residues instantly to 4°C to arrest spoilage bacteria.
Stage 02

Target Fraction Extraction & Separation

  • 03. SonFlow Free Flow Extraction: Heating solvent/water mixtures uniformly to release bound pectins or proteins.
  • 04. Decanter Centrifugation: Dividing solids-depleted bio-active liquor from exhausted spent fiber matrices.
Stage 03

High-Pressure Paste Pumping via ABEL HM

  • 05. ABEL Filter-Press Injection: Pumping thick fiber slurries up to 16 bar into presses to yield dry cake (35-40% DS).
  • 06. Biomass & Feed Upgrading: Converting compacted dry fiber cake into boiler biofuel or pelletized animal feed.
Stage 04 & 05

Solubles Evaporation & Mehrer Biogas Recovery

  • 07. SonFlow Vacuum Evaporation: Concentrating extracted bio-actives into high-purity pectin or polyphenol extracts.
  • 08. Anaerobic Digestion: Residual high-COD liquid fractions feed UASB reactors to generate green biogas.
  • 09. Mehrer 100% Oil-Free Biogas Booster: Compressing raw biogas reliably into plant boiler fuel headers.
2. The Integrated Side-Stream Valorisation Process Sequence
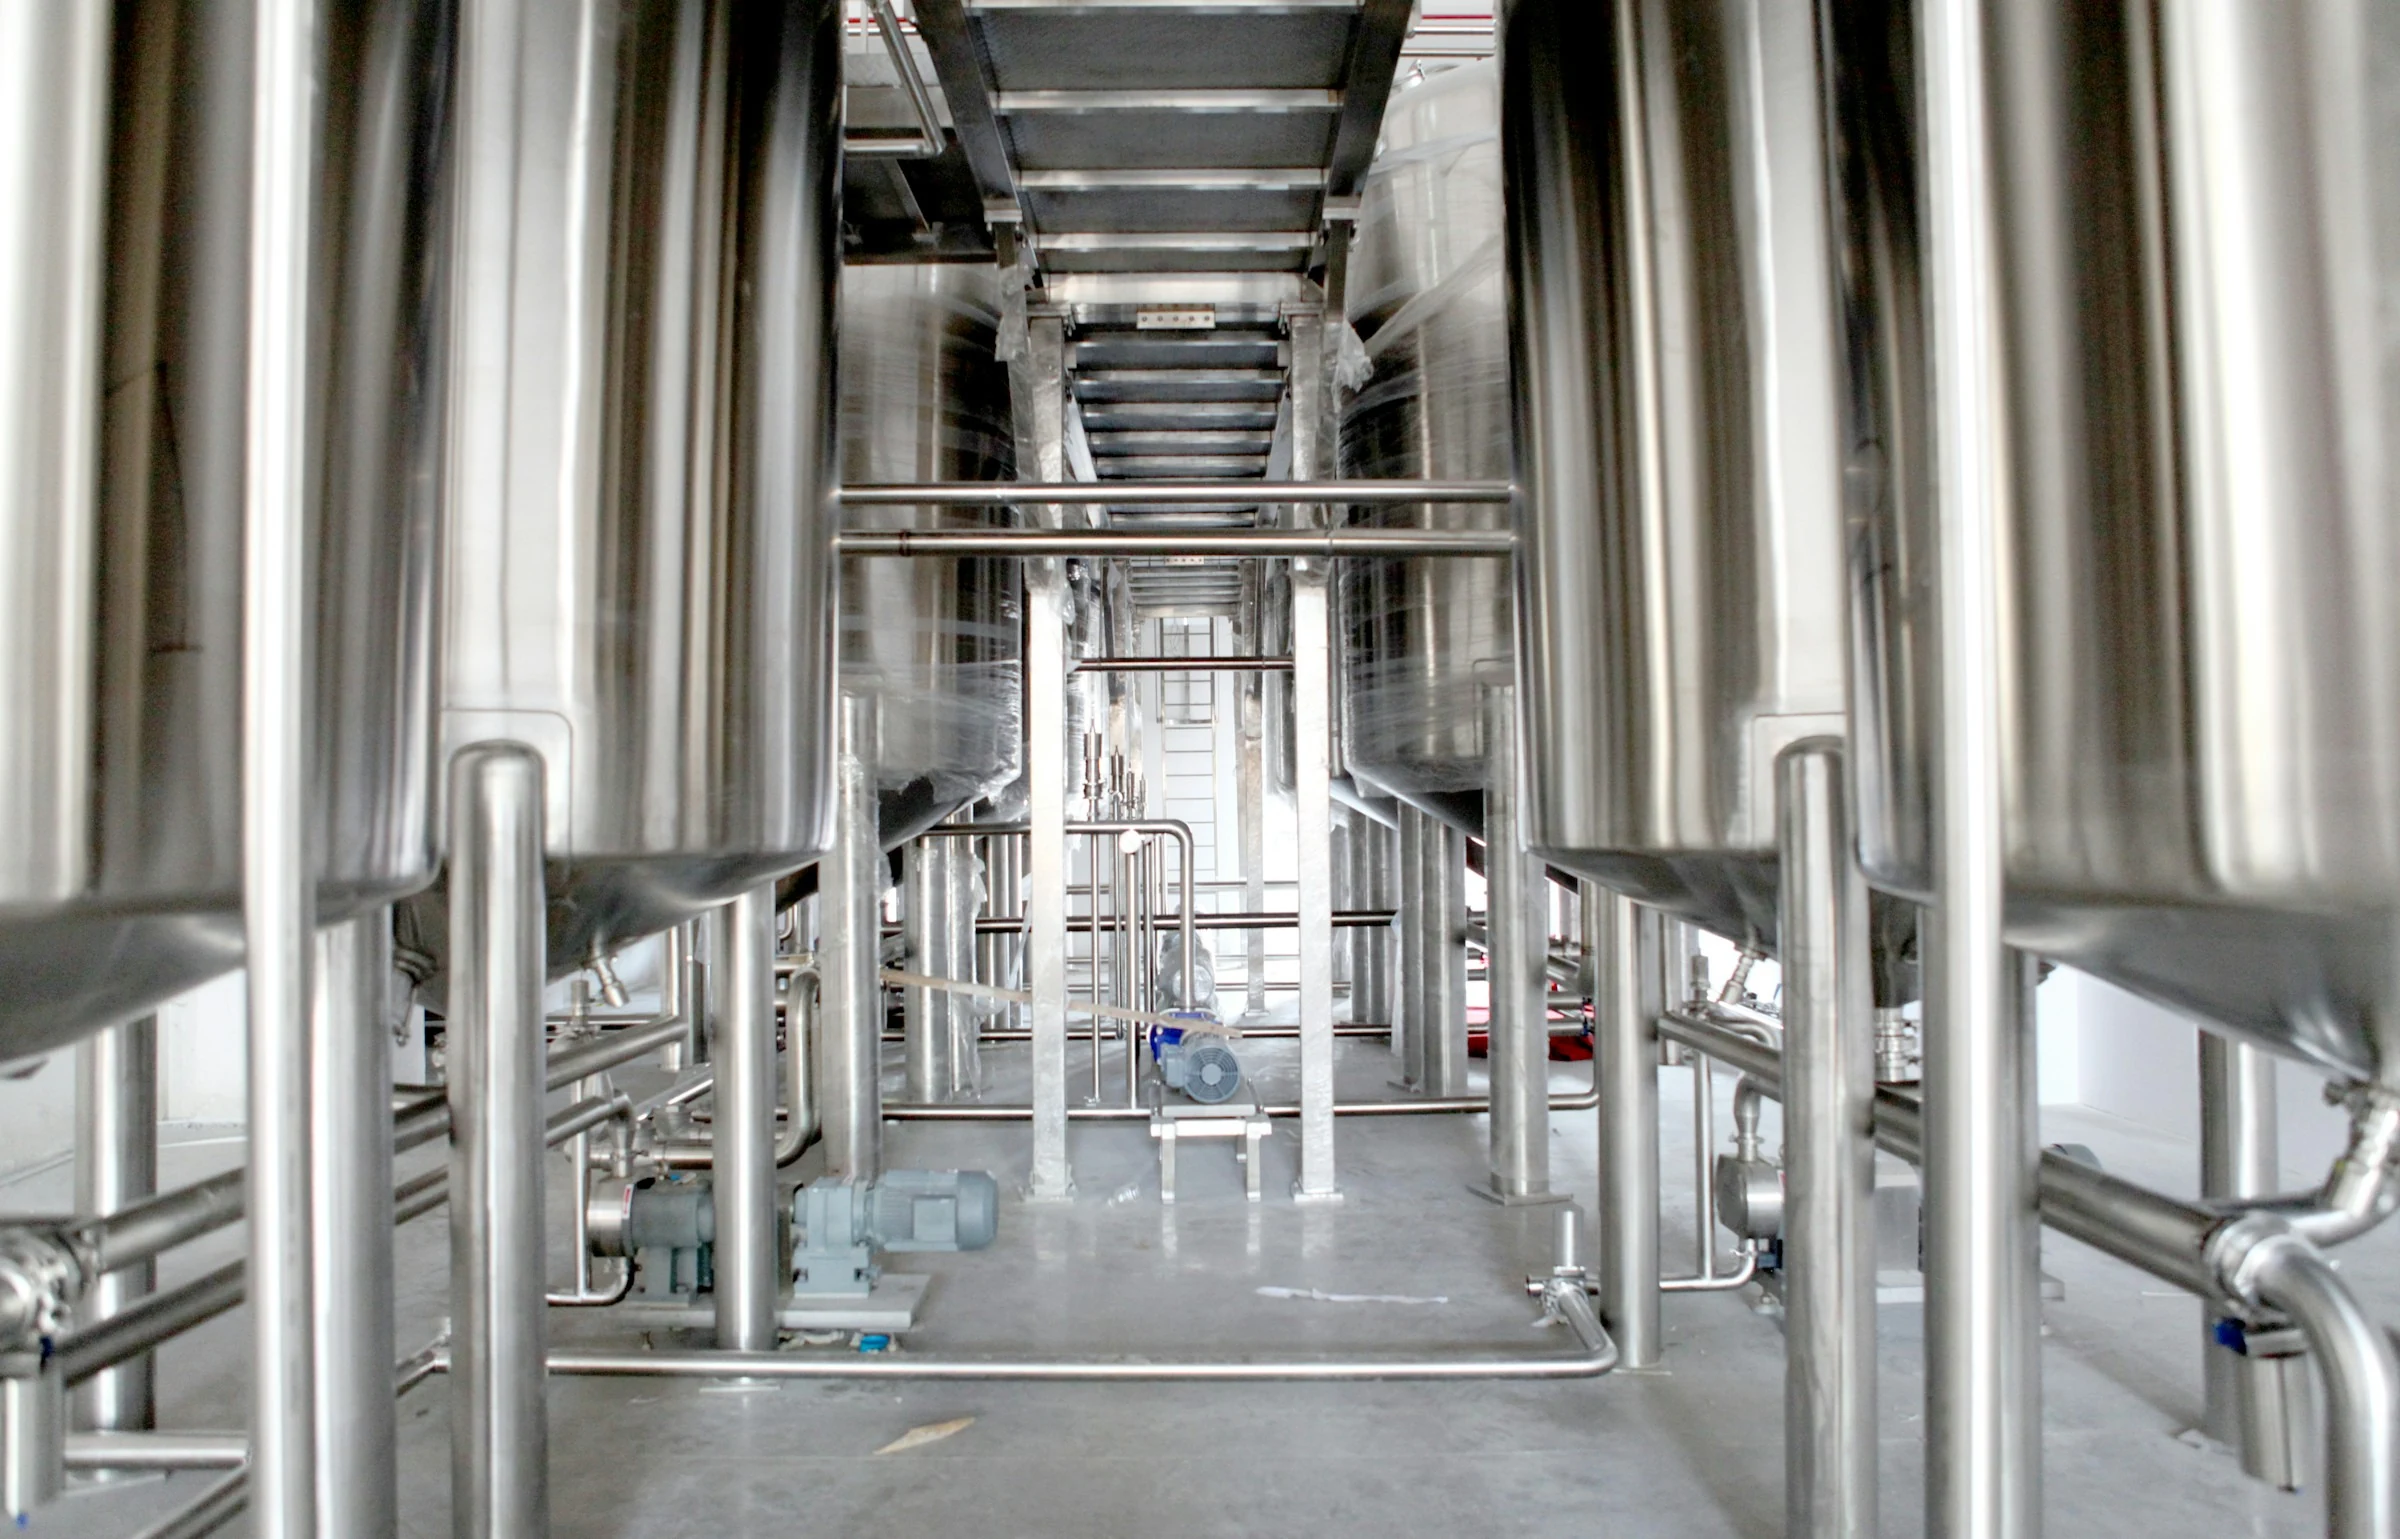
Fig 1.2: Bio-active extraction columns and integrated plate evaporation skids in a circular food valorisation facility.

3. Advanced Equipment Portfolio: SonFlow, ABEL & Mehrer

The tripartite European equipment synergy delivered by Lecoqimex masters the most demanding side-stream duties:

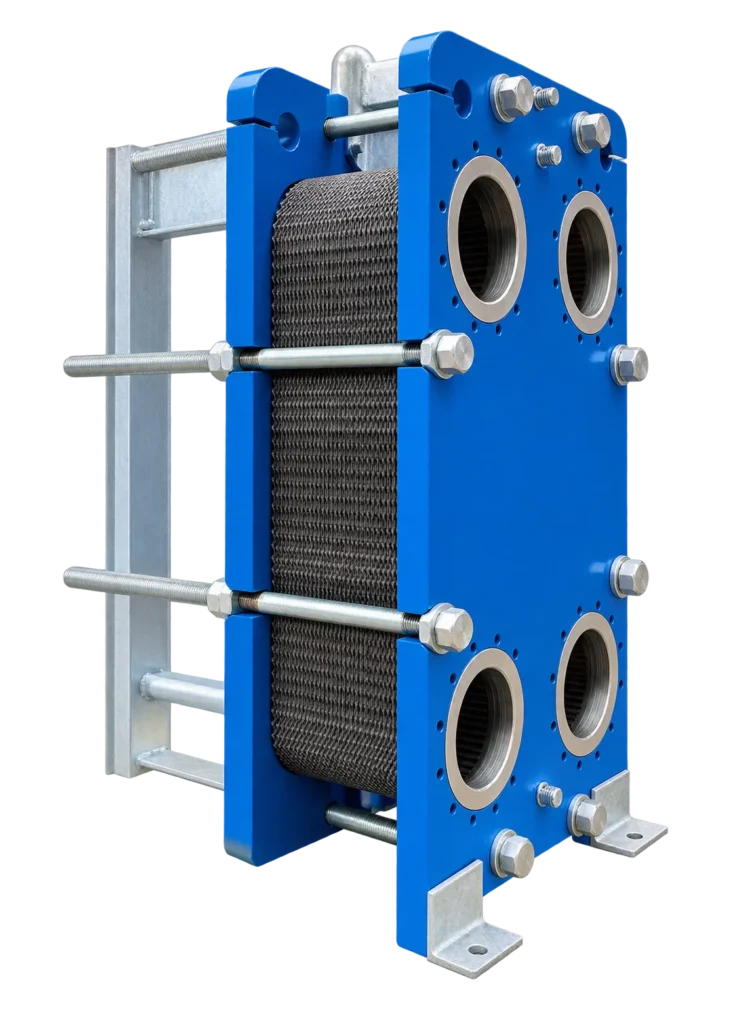
SonFlow Free Flow Plate Heat Exchangers

Generous open flow channels with zero plate contact points allowing fiber-laden bio-slurries to circulate freely without fouling or clogging.

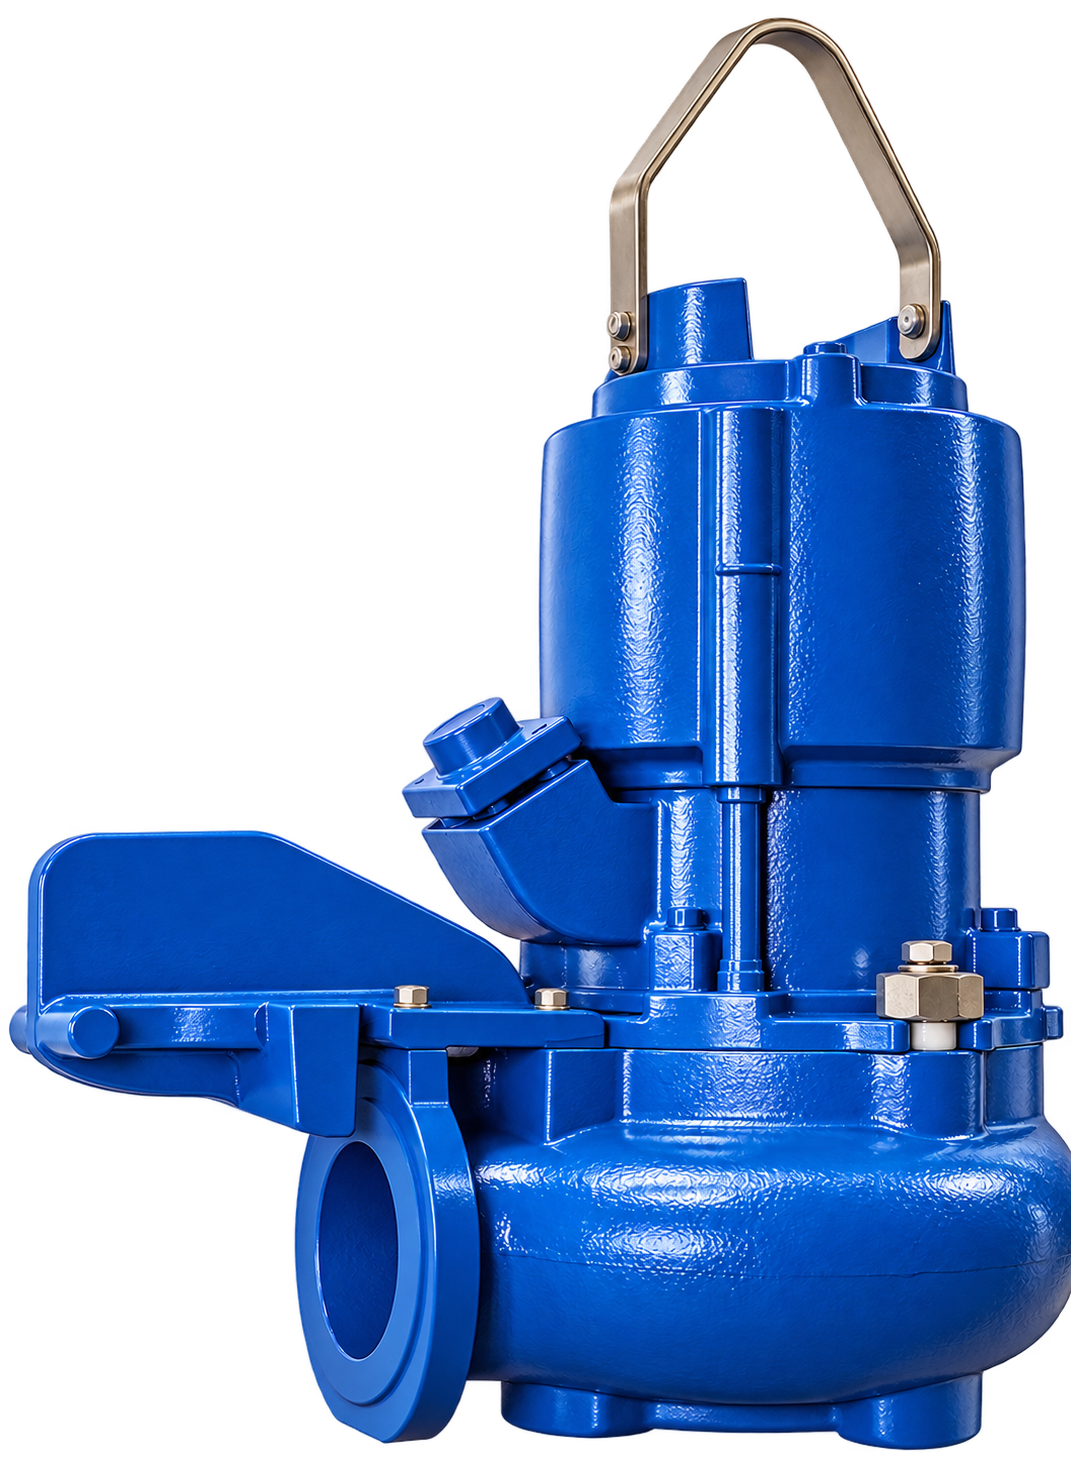
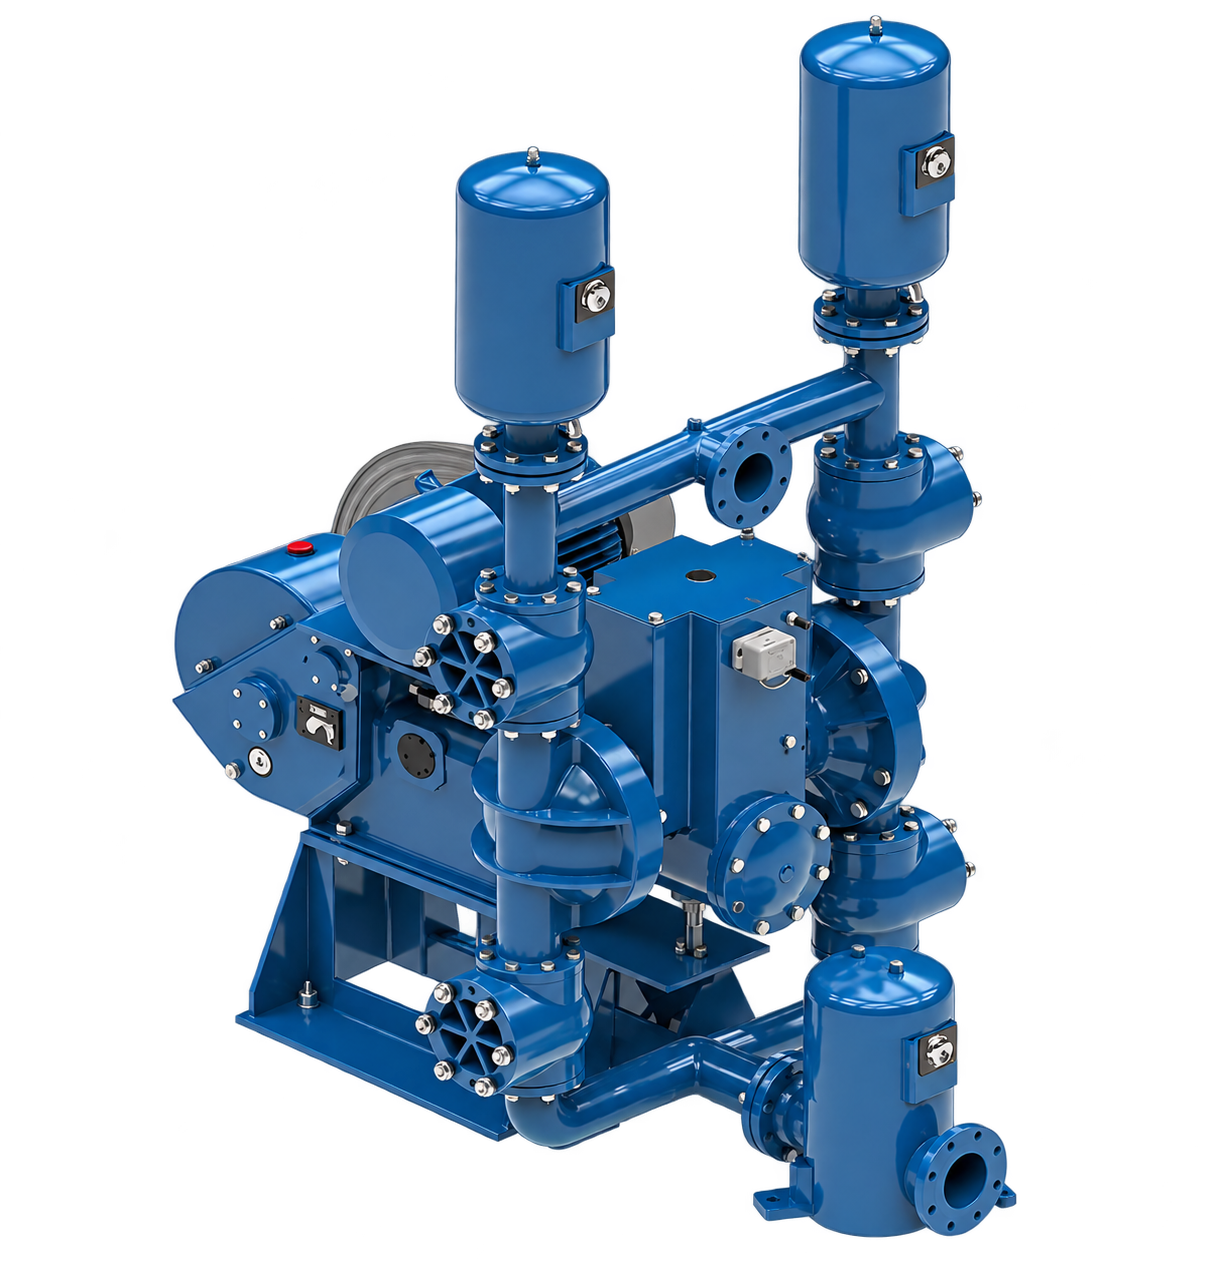
ABEL HM Heavy-Duty Piston Diaphragm Pumps

Purpose-built for viscous abrasive pastes. Generating up to 16-25 bar continuous injection pressure into filter presses to produce bone-dry cake.

Mehrer 100% Oil-Free Biogas Compressors

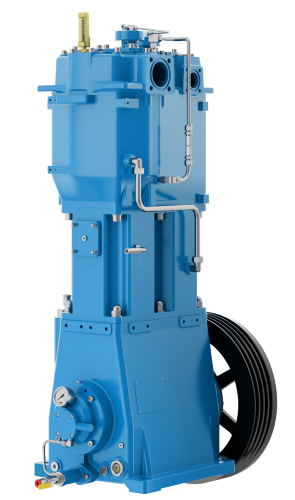
Dual-compartment crosshead construction keeping compression cylinders oil-free, compressing moist H2S-laden biogas safely for boilers.

SonFlow Vacuum Plate Evaporators

High heat transfer coefficients and low liquid hold-up protecting heat-sensitive bio-actives from thermal degradation during concentration.

3. Advanced Equipment Portfolio: SonFlow, ABEL & Mehrer
Fig 1.3: Heavy-duty ABEL HM pump skid and Mehrer oil-free gas compressor installed for food side-stream circular energy recovery.

Questions and answers about beer production solutions & equipment

Why does point-of-origin stream segregation dictate the viability of food valorisation projects?

Allowing pristine food side streams (such as spent brewers grain, sweet whey, or citrus peel) to mix into common floor drains alongside caustic CIP washes or washdown debris contaminates the stream with severe bio-burden and chemical toxins, permanently eliminating food- or feed-grade valorisation. Hygienic closed segregation at machine discharge protects biological purity, unlocking high-value ingredient extraction.

How does the SonFlow Free Flow plate heat exchanger operate reliably on coarse fibrous suspensions?

Extraction slurries derived from food pomace carry coarse cellulose fragments, seeds, and viscous pectinous gums. SonFlow Free Flow plates feature generous wide plate gaps (up to 12mm) and corrugation geometries engineered with zero metal-to-metal contact points along flow streamlines. Suspended solids and fibers glide through freely without bridging or entrapment, sustaining high thermal transfer rates.

What makes ABEL HM piston diaphragm pumps superior for moving thick dewatered pastes and cakes?

Thickened side-stream pastes leaving decanters or centrifuges exhibit high dry-solids concentrations (30-40% DS) and non-Newtonian plastic rheologies that completely stall standard centrifugal pumps. ABEL HM pumps combine reciprocating mechanical pistons hydraulically coupled to isolating membranes, generating continuous positive pressures up to 16-25 bar to push dense cakes through long-distance pipelines without mechanical wear.

Why are Mehrer 100% oil-free compressors specified for bio-methane gas recovery in food plants?

Raw biogas generated by anaerobic digestion of organic food residues contains methane, CO2, saturated water vapor, and corrosive traces of hydrogen sulfide (H2S). Mehrer compressors utilize a crosshead design with dual distance pieces completely separating the gas compression cylinder from crankcase lubrication. With zero oil in the gas stream, it eliminates lubricant contamination and prevents acid corrosion.

Technical Brochures, Manuals & Certificates

Discuss Your Food Side-Stream Valorisation & Circular Bio-Economy Project

From Free Flow plate exchangers for nutrient extraction and ABEL HM paste pumps to Mehrer 100% oil-free biogas compressors, Lecoqimex engineers calculate full economic feasibility.

Click to browse or drag files here
PDF, CAD, 3D STEP, Office, Images (Max 50MB)

Request for Quote Submitted Successfully!

Your technical dossier has been registered into the Lecoqimex engineering system.

B2B INQUIRY SLIP LIE-XXXX
LECOQIMEX
Integrated Industrial Solutions & OEM Spares
ELECTRONIC INQUIRY SLIP / SPEC RECORD
Ticket: LIE-XXXX
I. CLIENT & COMPANY INFORMATION
Full Name: --
Business Email: --
Phone Number: --
Company Name: --
Country / Location: --
II. SPECIFICATIONS & SCOPE
Technology Brand: --
Product / Model: --
Industry: --
Attached Documents: --
Current Status: Inquiry Received & Under Review
III. MESSAGE / REQUIREMENTS
--

How We Deliver Your Solution

From initial parameters to verified commissioning, our engineering team ensures optimal thermal performance and seamless integration.

01

Parameter Assessment

We analyze your specific flow rates, temperature profiles, wort gravity, and cellar cooling requirements.

02

Thermodynamic Modeling & CAD

Application engineers run thermodynamic simulations to size heat exchangers, select materials, and prepare 2D and 3D CAD files for your plant layout.

03

OEM Optimization & Proposal

You receive a detailed technical proposal with verified performance guarantees, energy recovery estimates, and transparent pricing.

04

Commissioning & Support

We provide on-site installation guidance, commissioning validation, full sanitary compliance documentation, and ongoing spare parts availability.

Need urgent sizing assistance? Reach our engineering team at +33 7 82 85 35 55 or services@lecoqimex.com

Link copied!