Commercial brewing
World-class commercial brewing expertise and equipment — developed over decades of European engineering — enabling breweries to produce consistent, high-yield beer at scale.
Explore Process Stage →Beer production is continually evolving as customer tastes shift and product variety expands. What remains constant is the drive to make great beer while saving on costs, water and energy in this resource-intensive industry. Lecoqimex delivers world-class European thermal, gas compression, and sanitary fluid technologies to empower brewery operations — from pioneering craft breweries to large-scale commercial facilities.
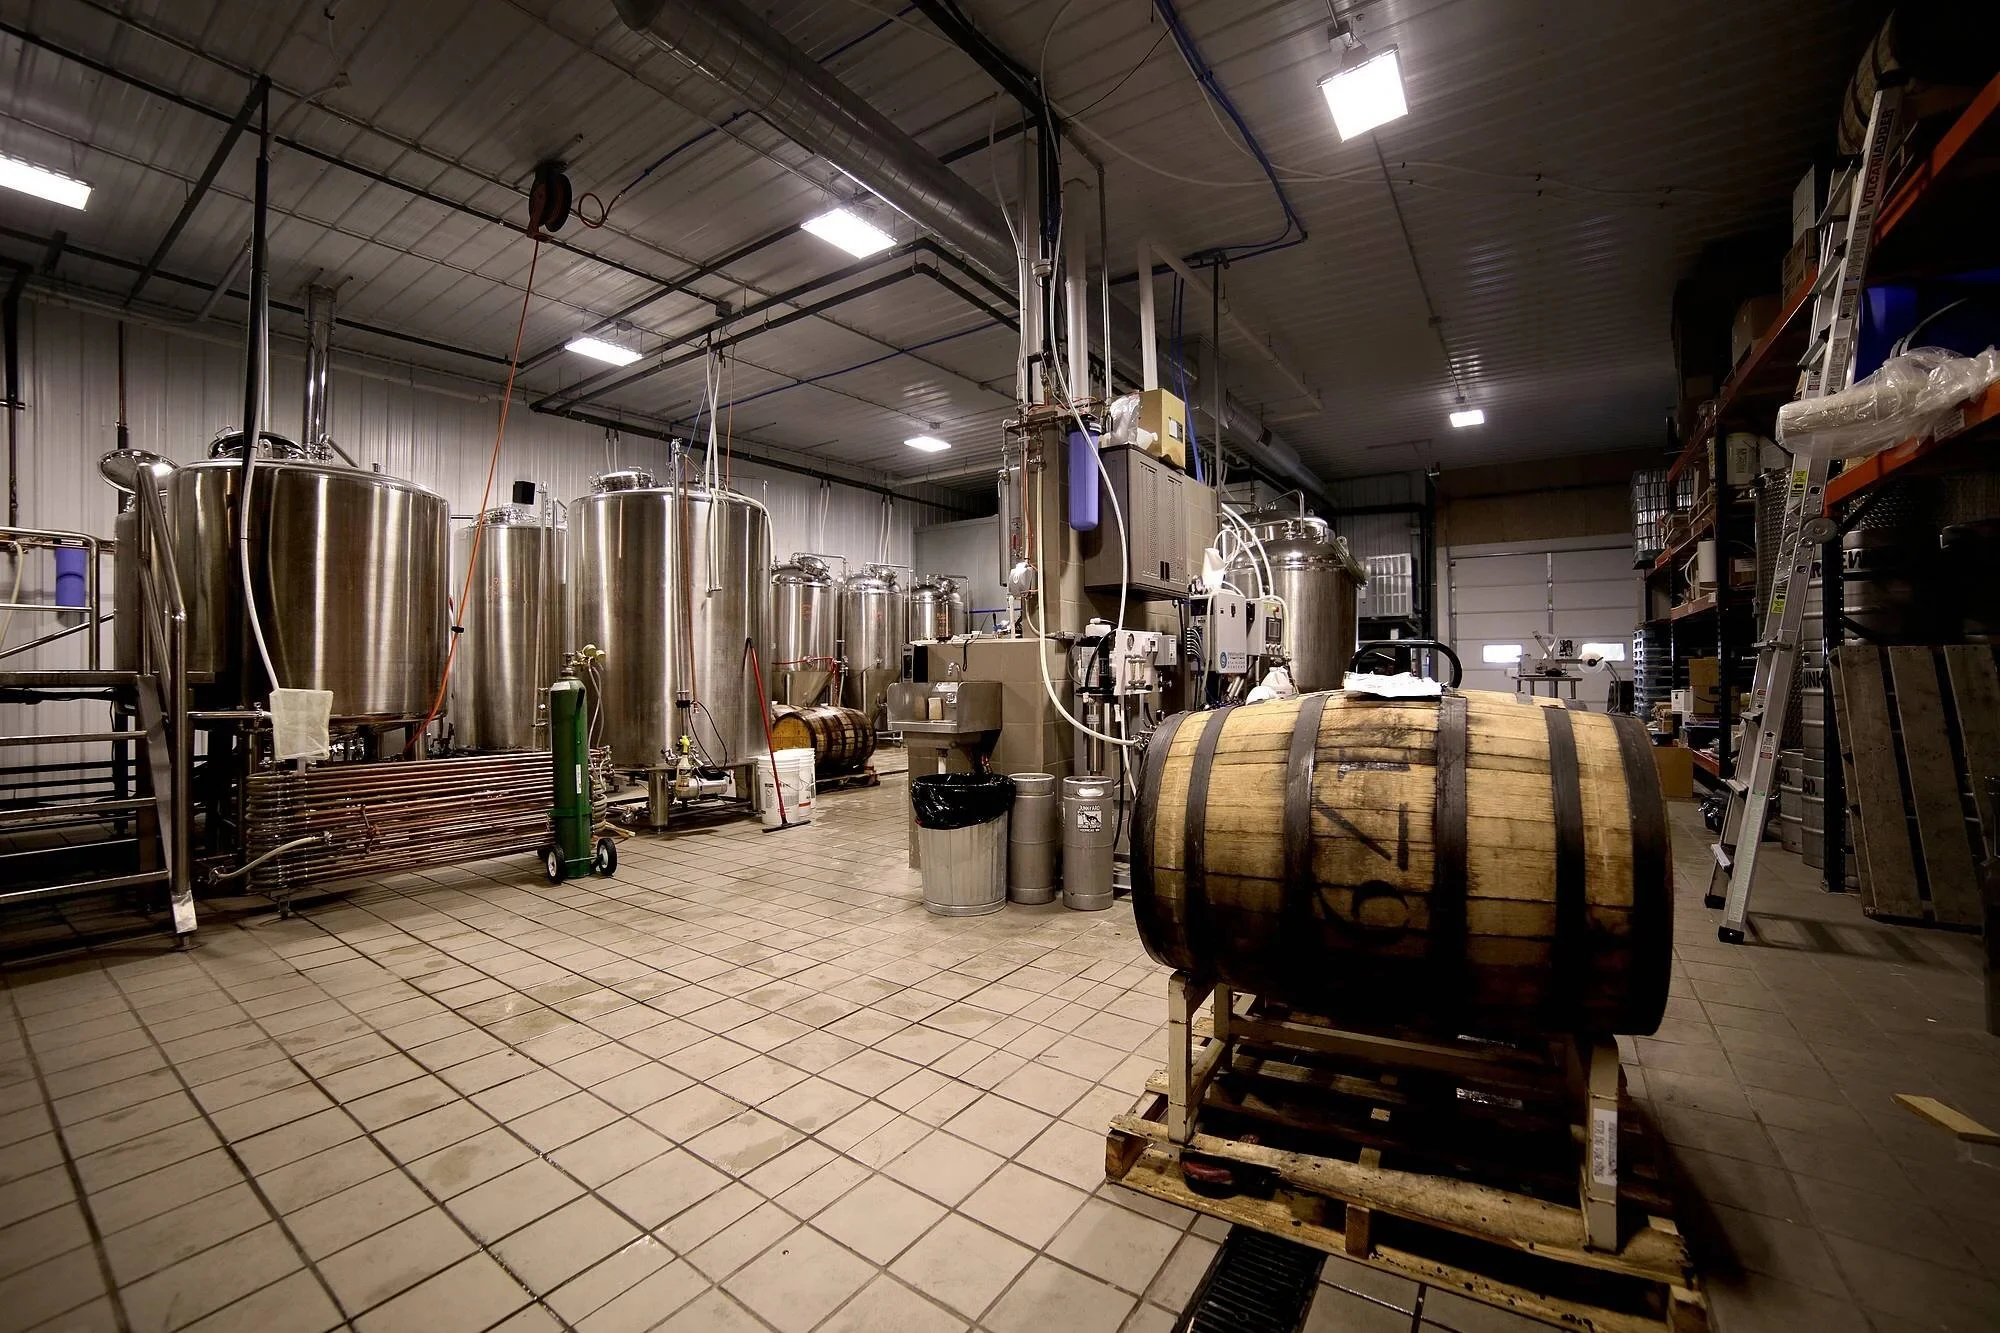
Whether it's for the benefit of the world's largest commercial beer producers or for a family-run craft brewery, Lecoqimex has the know-how and technologies to enable customers to deliver a high-quality beverage, while achieving profitable operations that save on water and energy. Lecoqimex understands that energy efficiency and responsible water stewardship are central to brewing operations and leverages decades of European OEM integration to pioneer a positive impact with unrivaled technology and service.
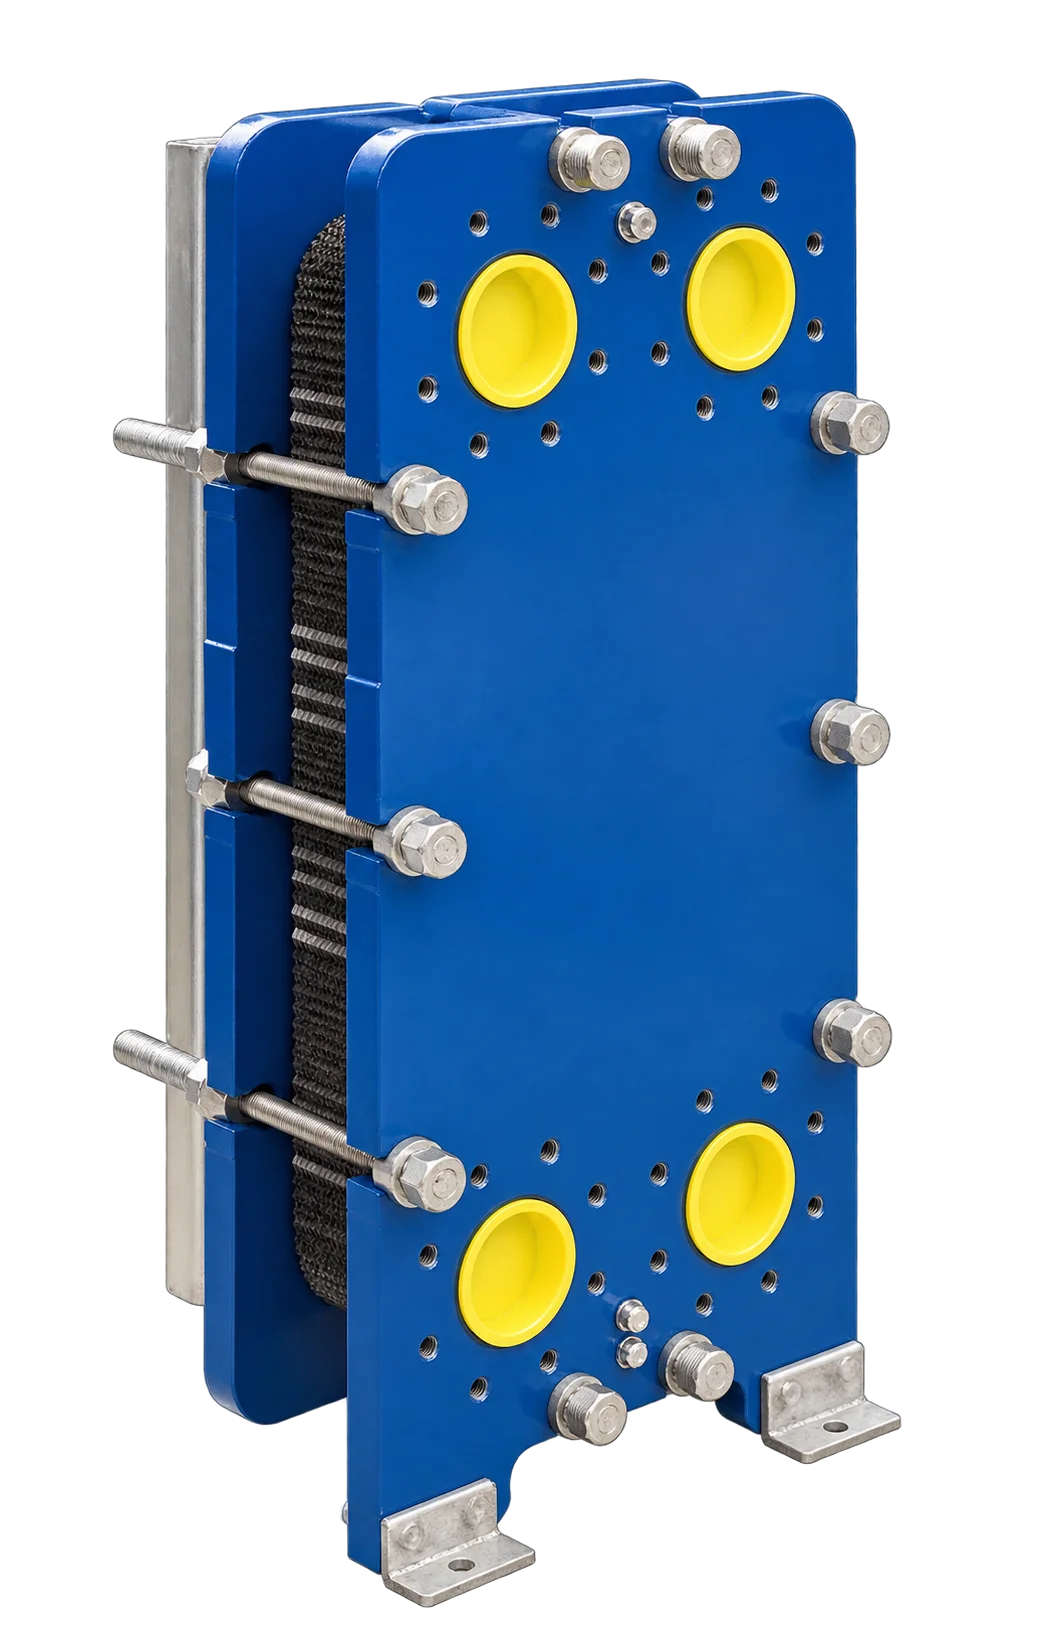
SonFlow 3-A certified sanitary gasketed plate heat exchanger engineered for precise two-stage wort cooling and cellar fermentation temperature regulation.
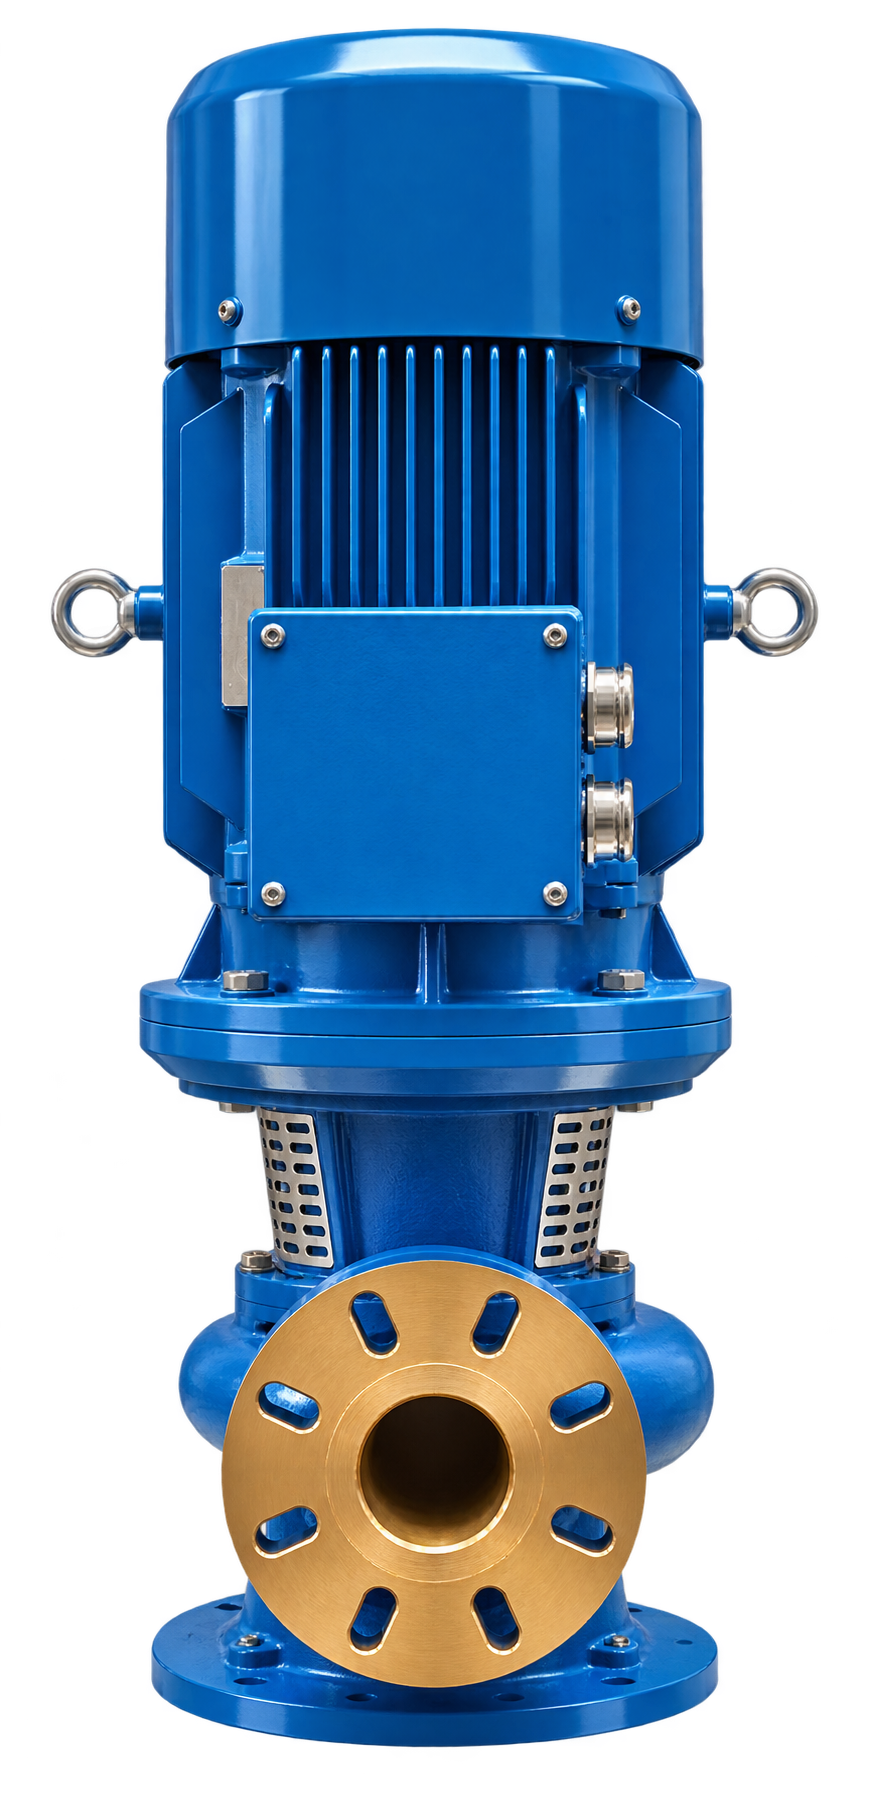
DanPumps in-line centrifugal circulation pump delivering steady, low-noise hydraulic flow across brewery cellar glycol cooling loops and hot water mains.
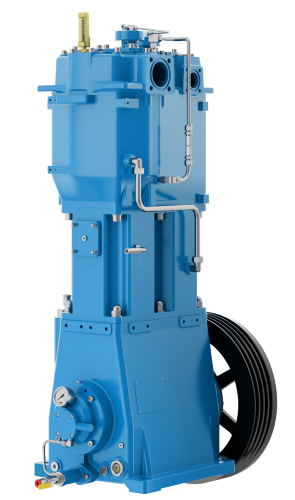
Mehrer 100% oil-free reciprocating compressor with dual crosshead distance pieces, recovering food-grade fermentation CO2 for carbonation and bottling lines.
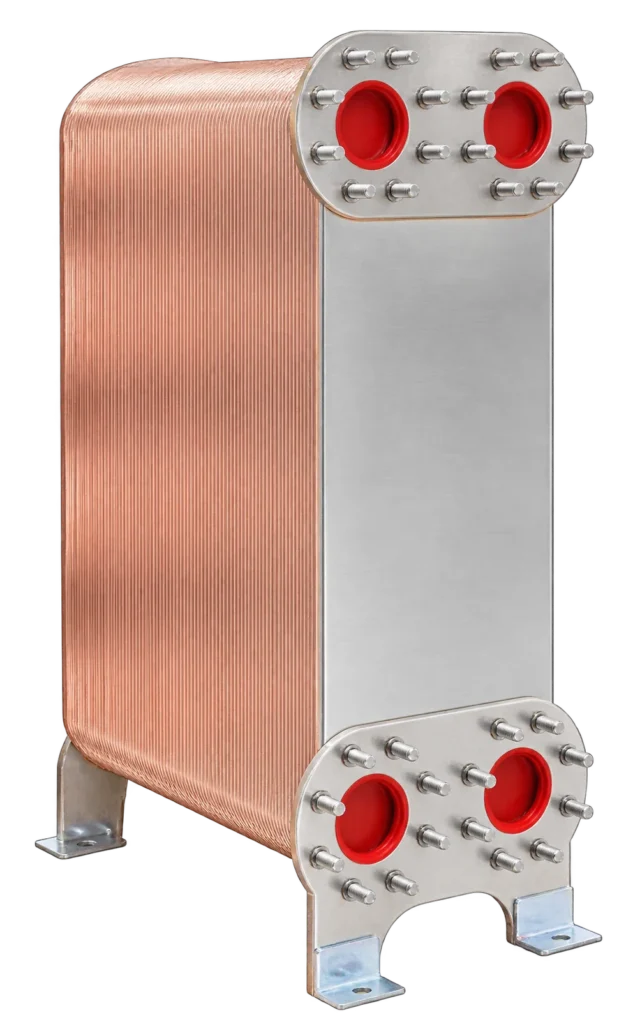
Compact SonFlow copper-brazed plate heat exchanger rated for 40 bar working pressure, optimal for brewery glycol chilling skids and flash cooling loops.
World-class commercial brewing expertise and equipment — developed over decades of European engineering — enabling breweries to produce consistent, high-yield beer at scale.
Explore Process Stage →
Lecoqimex partners with independent craft brewers, providing compact sanitary PHEs, cellar cooling and support to help them innovate, expand, and share a passion for great beer.
Explore Process Stage →There are no insights to display at the moment. Please check back later.
Breweries can improve reproducibility through automated process control for separation, yeast handling, carbonation, and blending. This helps ensure consistent quality, flavour, clarity, and alcohol content across batches while providing the flexibility to adapt processes for seasonal and specialty beers. Sanitary brew centrifuges and plate heat exchangers support consistency by removing solids without filtration or oxygen pickup, improving yield and helping preserve the character of beers ranging from clear lagers to hazy IPAs.
High hop, ingredient-rich, and specialty beers require precise control of solids, haze, and oxygen. Our engineered solutions help breweries manage hop extraction, mixing, contact time, and beer recovery, enabling consistent quality, higher yield, and efficiency.
Breweries can accelerate production by reducing clarification and maturation time. Sanitary craft brew centrifuges help accelerate the transition from fermentation to finished beer while freeing up tank capacity, and inline carbonation supports faster production with consistent quality.
Breweries can expand their product portfolio with de-alcoholization technologies that enable the production of low-alcohol, no-alcohol, and other fermented beverages while preserving flavour, aroma, and mouthfeel. We offer membrane filtration and stripping-based solutions, helping breweries efficiently enter and scale in the growing low- and no-alcohol market.
Consistent yeast management, clarification, and hygienic processing help breweries maintain flavour stability, product quality, and shelf life. Our solutions support reliable brewing through efficient clarification, yeast management, and hygienic processing, helping breweries achieve consistent flavour, improved shelf life, reduced product loss, and high-quality results batch after batch.
Breweries gain flexibility through process solutions that support different beer styles and production goals. Our portfolio includes centrifuges for gentle beer clarification, yeast management systems for consistent fermentation, dry hopping solutions for controlled hop extraction, inline carbonation for precise carbonation, and de-alcoholization technologies for low- and no-alcohol beverages. Together, these solutions help breweries innovate faster while maintaining quality, consistency, and production efficiency across a wide range of products.
Breweries can reduce energy use through heat recovery and energy-efficient process technologies. Key opportunities include wort boiling, cooling, separation, and de-alcoholization.
For example, heat recovery from wort vapour pre-heats the next batch, reducing steam consumption by up to 10%, and high-efficiency plate heat exchangers recover up to 90% of available thermal energy, achieving energy consumption below 0.4 kWh/hl.
Share your brewhouse hectoliter capacity, wort cooling profile, or CO2 recovery flow rate with our brewery engineering specialists.
Your technical dossier has been registered into the Lecoqimex engineering system.
 LECOQIMEX
From initial parameters to verified commissioning, our engineering team ensures optimal thermal performance and seamless integration.
We analyze your specific flow rates, temperature profiles, wort gravity, and cellar cooling requirements.
Application engineers run thermodynamic simulations to size heat exchangers, select materials, and prepare 2D and 3D CAD files for your plant layout.
You receive a detailed technical proposal with verified performance guarantees, energy recovery estimates, and transparent pricing.
We provide on-site installation guidance, commissioning validation, full sanitary compliance documentation, and ongoing spare parts availability.
Need urgent sizing assistance? Reach our engineering team at +33 7 82 85 35 55 or services@lecoqimex.com